Primary Cold-Drawn Wire Rods & Structural Solutions (Group A)
Immediate dispatch available from our 1,500-acre Daqiuzhuang (Tianjin) and Tangshan manufacturing clusters. Below are 8 core lines certified for global engineering contracts.
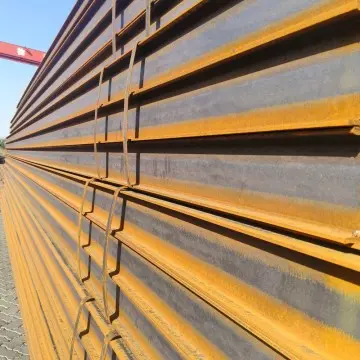
A36 / Q235 Grade Structural H-Beam
Heavy structural columns and wide-flange beams matching EN 10025-2 S235JR and ASTM A36 for workshop platforms, high-rises, and industrial frames.
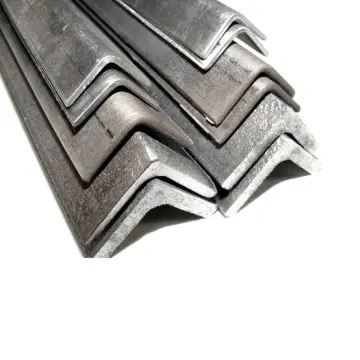
Perforated Galvanized Angle Steel
Equal and unequal slotted angle bars designed for bolted assembly racks, offshore staging, cable tray bridges, and modular solar frameworks.
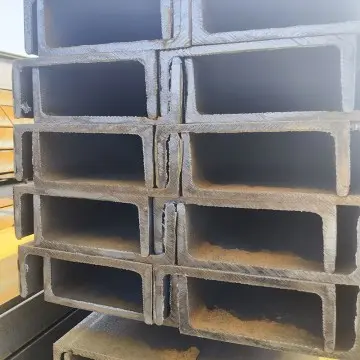
Galvanized C/U Channel Steel
Standard hot-rolled structural steel channels offering superior resistance to torsional bending in purlins, automotive subframes, and bridges.
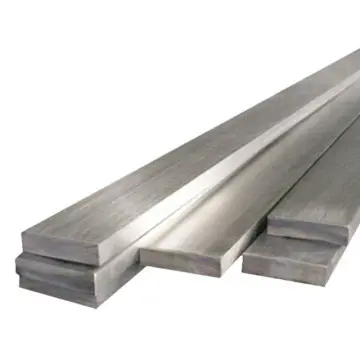
Q235B Carbon Steel Flat Bar
Precision-sheared and slit flat bars utilized extensively for earthing grids, agricultural fabrication, structural gussets, and machine base plates.
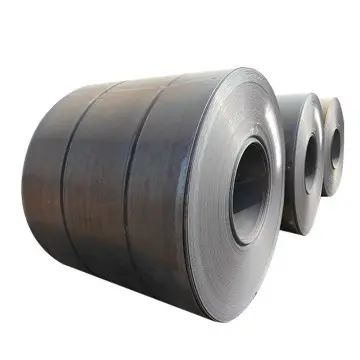
HR & CR Carbon Steel Coils
Clean surface pickled and oiled (P&O), cold-rolled fine-finish steel coils tailored for ERW pipe manufacturing, stamping, and metal profiling.
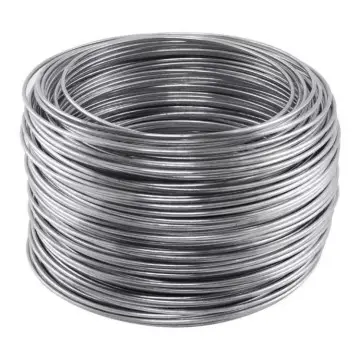
SAE1080 / Q235 Wire Rod in Coils
Feedstock wire rods for deep drawing into CO2 gas shielded solid welding wires (AWS ER70S-6), submerged arc flux-cored wires, and cold heading.
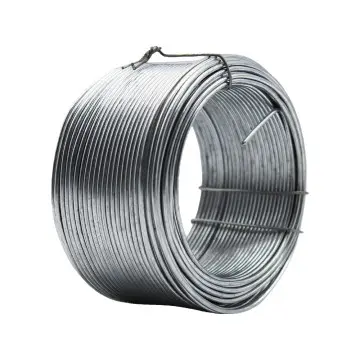
SAE1006 / SAE1008 Cold Drawn Wire
Micro-alloyed smooth drawn bright wire engineered for high-speed continuous nail making, automated mesh welding, and precision rod re-drawing.
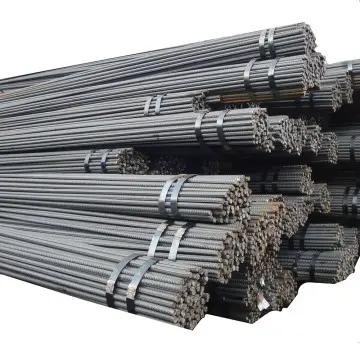
Deformed Steel Rebar (6mm – 12mm)
High-yield deformed rebars (HRB400 / HRB500 / BS 4449 Gr 500B) for foundation piles, deep marine substructures, and civil precast elements.
Engineering Principles of CE Certified Cold-Drawn Electrode Wire Rods
Navigating EU Construction Products Regulation (EU CPR 305/2011), Harmonized Standard EN 13479, and Precision Metallurgy for Continuous Robotic Welding Consumables.
Mandatory EN 13479 & System 2+ Verification
In the European Union and member economic zones, welding consumables used in steel and aluminum structural fabrication are classified under Construction Products Regulation (CPR 305/2011). Under standard EN 13479: Welding consumables — General product standard for filler metals and fluxes for fusion welding of metallic materials, manufacturers cannot self-certify. An accredited Notified Body (NB) must conduct initial inspection of the Factory Production Control (FPC) system and maintain continuous surveillance under System 2+ verification, issuing an official CE Certificate of Conformity for every melt heat.
Cold-Drawing Physics & Surface Lubricity
Cold drawing of electrode wire rods transforms hot-rolled raw stock (typically 5.5mm or 6.5mm) through progressive tungsten carbide or poly-crystalline diamond dies down to 0.8mm, 1.0mm, 1.2mm, or 1.6mm. The cold plastic deformation generates work-hardening, elevating tensile strength to 500–1200 MPa while preserving crucial microstructural ductility. Modern high-speed automatic lines require strict ovality tolerances (under ±0.01mm) and residual drawing lubricant control (<0.12 g/m²) to guarantee stable electrical contact tip transfer without nozzle clogging.
Chemical Deoxidation & Hydrogen Control
Electrode rods conforming to grades like AWS A5.18 ER70S-6 or EN ISO 14341-A G 42 4 M21 3Si1 necessitate balanced Silicon (0.80%–1.15%) and Manganese (1.40%–1.85%) proportions. These elements serve as active deoxidizers against atmospheric entrapped oxygen and carbon monoxide porosity during shielding gas burn. Strict vacuum degassing (RH/VD) in our blast furnace facilities guarantees diffusible hydrogen levels below H5 (5 ml/100g deposited weld metal), mitigating cold-cracking hazards in structural heavy-wall steel.
| Classification Standard | Grade Designation | Yield Strength (MPa) | Tensile Strength (MPa) | Min. Charpy-V Impact | Primary Industrial Use |
|---|---|---|---|---|---|
| EN ISO 14341-A (CE) | G 42 4 M21 3Si1 | ≥ 420 MPa | 500 – 640 MPa | ≥ 47 J at -40°C | Bridges, Cranes, Structural Frames |
| AWS A5.18 (USA) | ER70S-6 | ≥ 400 MPa | ≥ 480 MPa | ≥ 27 J at -29°C | Automotive, Pressure Vessels, Tubing |
| GB/T 8110 (China) | ER50-6 (Q235/Q355) | ≥ 420 MPa | 500 – 620 MPa | ≥ 47 J at -30°C | Heavy Engineering Machinery, Rail |
| EN ISO 24912 / SAW | S2Mo / EM12K | ≥ 470 MPa | 550 – 680 MPa | ≥ 47 J at -20°C | Submerged Arc Wind Tower Welding |
| SAE/AISI Low Carbon | SAE 1006 / 1008 | ≥ 210 MPa | 350 – 480 MPa | N/A (Forming) | Nails, Binding Wire, General Redrawing |
Why Global Tier-1 Contractors Source from HZXY & North China Hubs
Combining 30 years of smelting mastery, fully localized raw material clusters in Daqiuzhuang and Tangshan, and deep intermodal access to Tianjin International Port.
Cluster Synergies in Daqiuzhuang & Tangshan
Headquartered in Daqiuzhuang, Tianjin, with dual rolling facilities in Tangshan spanning 1,500 acres, HZXY benefits from China's dense blast-furnace and billet supply matrix. Molten iron, scrap feeding, continuous casting, and rough drawing take place within a 60-kilometer logistics radius, eliminating inland hauling premiums and yielding raw material cost advantages of 12% to 18% over fragmented European re-rollers.
10 Million+ Metric Ton Annual Output
Scale guarantees supply security. Unlike boutique drawing shops susceptible to single-line downtime, our facility groups operate 34 automated wire drawing blocks, multiple inline gas galvanizing lines, and specialized copper-coating baths. We fulfill 5,000-ton bulk EPC wire rod allocations within tight project schedules, shielding overseas buyers from spot commodity price spikes.
Port Proximity & One-Stop Bill of Materials Consolidation
Located under 70 km from Tianjin Port (the premier container and break-bulk gateway of North China), shipping transit times to Europe, the Middle East, Southeast Asia, and the Americas are minimized. Furthermore, project buyers can combine electrode wire rods with H-beams, hollow sections, galvanised pipes, rebar, and industrial valves in a consolidated Bill of Materials (BOM) container pack, saving thousands in freight and port clearance fees.
Comprehensive Cost Drivers & Enterprise Quotation Formulation
Demystifying how international tier-1 quotes are built: metallurgical chemistry, copper vs. non-copper coating, spooling dynamics, and Incoterm logistics.
1. Raw Wire Rod Chemistry Grade & Premium Alloys
The initial pricing benchmark begins with the steel base index (e.g., Tangshan Q235B or high-grade SAE1006 / ER70S-6 billet). Clean molten steel deoxidized with higher Mn/Si balance incurs a refining cost of $25–$45/ton above standard carbon wire, ensuring low spatters and consistent tensile properties.
- Low Impurity Tolerance: P < 0.025%, S < 0.025%, Cu < 0.20%.
- Micro-Alloying: Targeted additions of Ti, Zr, and Al for grain refinement.
2. Surface Treatment: Copper Coated vs. Copper-Free
Traditional MIG wires receive a chemical or electrochemical micro-copper flash (0.05%–0.20% by weight) to safeguard against atmospheric oxidation and boost current feedability. Copper-free environmental wire rods, processed using specialized micro-thin protective organic coatings, eliminate copper fume toxicity during high-amperage welding.
- Copper Flash Coating: Standard economical option for manual & GMAW.
- Polished Green/Copper-Free: Zero copper flaking, optimal for robotic cells.
3. Packaging, Spooling & Payoff Drum Automation
Bulk coils (catch-weight coils 800–1,000 kg) are priced at base rate. Precision level-layer-wound plastic/metallic spools (D270, D300, 15 kg/spool) or heavy automated robotic Marathon drums (250 kg & 350 kg) with anti-twist feeding systems incur precision winding costs ($40–$70/ton).
- Robotic Drums (250-350kg): Eliminates downtime in robotic automotive plants.
- VCI Vacuum Anti-Rust Film: Guaranteed 24-month marine transit protection.
4. Incoterms, Compliance Testing & Freight Optimization
Export quotes from HZXY clearly demarcate FOB Tianjin, CIF Rotterdam, CFR Hamburg, or DDP destination project staging yards. Quotes incorporate EN 10204 Type 3.1 chemical & physical certification costs, notified body batch inspection (SGS, TÜV, Bureau Veritas), and customs tariffs.
- Direct Shipping: Loading directly via Tianjin Port break-bulk/FCL.
- Transparent Terms: Letter of Credit (L/C), T/T, and open account flexibility.
Mission-Critical Sectors Built With Certified Welding Rods
From offshore wind turbine substructures to monumental high-speed rail viaducts, our cold-drawn electrode rods undergo severe low-temperature impact tests to prevent structural fatigue.
Offshore Wind & Marine Megastructures
Offshore wind jackets, monopiles, and marine FPSO vessels demand weld seams that endure constant cyclic fatigue in freezing saltwater environments. Our CE-marked electrode wires achieve Charpy V-Notch toughness exceeding 47 Joules at -40°C, meeting DNV, ABS, and Lloyd’s Register offshore shipbuilding requirements.
High-Pressure Boilers & Energy Pipelines
Cross-country natural gas pipes and steam thermal generation boilers require seamless joint penetration under radiographic and ultrasonic testing. Our strictly drawn low-diffusible hydrogen (H5/H4) welding rods safeguard longitudinal and circumferential seams from micro-porosity and brittle cleavage fractures.
Automotive Chassis & Heavy Earthmoving Fleet
High-speed robotic GMAW welding stations in automotive unibody and heavy excavator boom fabrication demand flawless wire feeding consistency. With our wire diameter tolerance maintained strictly under ±0.01 mm, arc wander and feed-motor slip are entirely eradicated across multi-shift production cycles.
Technological Innovations Reshaping the Global Electrode Market
Key developments driving higher productivity, lower lifecycle emissions, and deeper automation across the welding industry.
1. Low-Carbon Steel & CBAM Decarbonization
With the European Union Carbon Border Adjustment Mechanism (CBAM) coming into full financial effect, importers must report embedded emissions. HZXY is transitioning major drawing furnaces to electric arc furnace (EAF) lines powered by regional green grid energy and waste-heat recovery systems, lowering the carbon footprint per ton of exported cold-drawn wire to secure lower carbon border levies.
2. Fully Copper-Free Robotic Solid Wires
Occupational safety mandates across North America and Europe are curbing copper dust accumulation within enclosed robotic manufacturing cells. Non-copper coated wires, calibrated with proprietary non-metallic lubricants, provide cleaner air for fabrication teams and significantly prolong welding torch liner longevity by eliminating copper abrasive wear.
3. Advanced Laser-Arc Hybrid Consumables
As shipbuilding and container fabrication pivot to combined laser-GMAW hybrid welding, cold-drawn wire rods require even tighter metallurgical homogeneity. Specialized micro-alloyed electrode chemistries stabilize the laser-induced keyhole vapor plume, boosting welding speeds upwards of 2.5 meters per minute without root undercut.
Frequently Asked Questions for Project Engineers & Buyers
Clear, authoritative technical answers on certifications, order batching, testing standards, and logistics.
What exact documents verify that cold-drawn electrode wire rods comply with EU CE Certification?
- CE Certificate of Conformity for Factory Production Control (FPC): Issued by a recognized European Notified Body under EN 13479:2017 System 2+.
- Declaration of Performance (DoP): Issued directly by the manufacturer, specifying essential mechanical, chemical, and elongation characteristics.
- EN 10204 3.1 Mill Test Certificate (MTC): A lot-specific inspection certificate proving chemical composition (C, Si, Mn, P, S, Ni, Cr, Mo, V, Cu), yield, tensile, and Charpy impact values.
How does HZXY control cast-to-cast chemical consistency for high-speed automated welding?
Can overseas buyers combine electrode wire rods with other construction steel materials in one order?
What is the typical lead time for custom spooling (15kg plastic vs. 250kg automated drum)?
Are third-party pre-shipment inspections (SGS, TÜV, Bureau Veritas) permitted at your Tianjin base?
What are the key price benchmarks to monitor when requesting quotes for cold-drawn wire rods?
Essential Structural, Pipeline & Tubular Steel Lines (Group B)
Manufactured in Tianjin and Tangshan to international ASTM, EN, and JIS benchmarks. Explore our additional 8 best-selling product categories for consolidated global procurement.
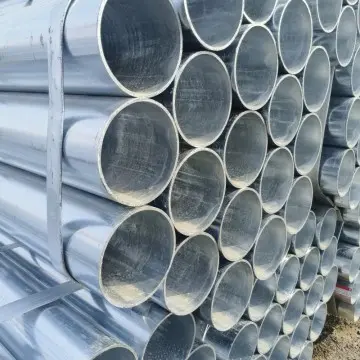
Galvanized Scaffolding Pipe
High-strength round structural tubing for modular scaffolding, temporary support towers, and agricultural greenhousing frames.
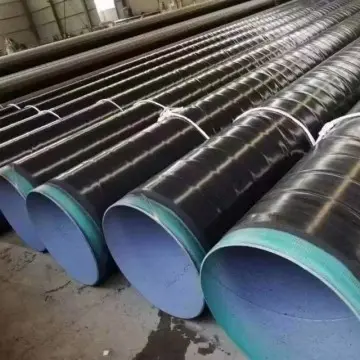
Anti-Corrosion Industrial Pipe
Polyethylene 3LPE, epoxy-coated, and hot-dip galvanized steel pipes designed for subsea discharge, municipal utilities, and mining slurries.
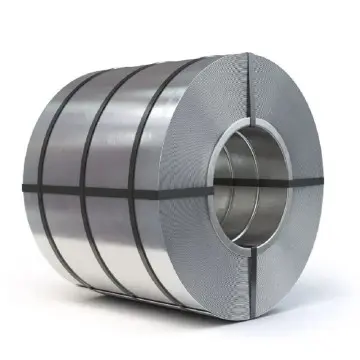
DX51D–DX54D Galvanized Coil
Continuous hot-dip galvanized steel coils (Z40 to Z275) optimized for HVAC ducting, cable trays, and structural cladding.
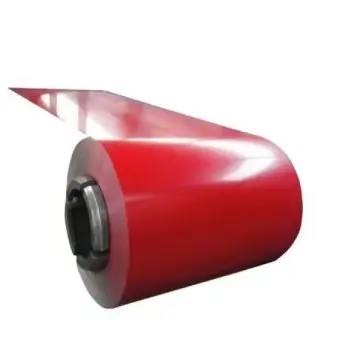
Prepainted PPGI / PPGL Coils
Double-baked architectural coil sheets in vibrant RAL colors with high UV resistance for industrial roofing and sandwich wall panels.
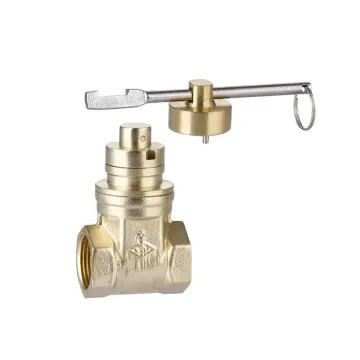
Pressure-Resistant Valves
Cast iron and stainless gate, butterfly, globe, and check valves matched directly to our steel pipeline schedules for complete MEP integration.
Solid Square Steel Bar
Solid forged and hot-rolled square bars utilized in heavy machinery shafts, ornamental architectural railings, and security grilles.
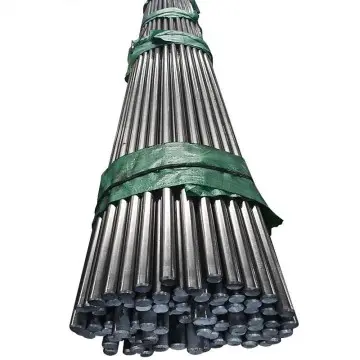
Galvanized Plain Round Bar
Corrosion-proof smooth carbon bars for bridge expansion dowel rods, chemical anchor bolts, and offshore rigging hardware.
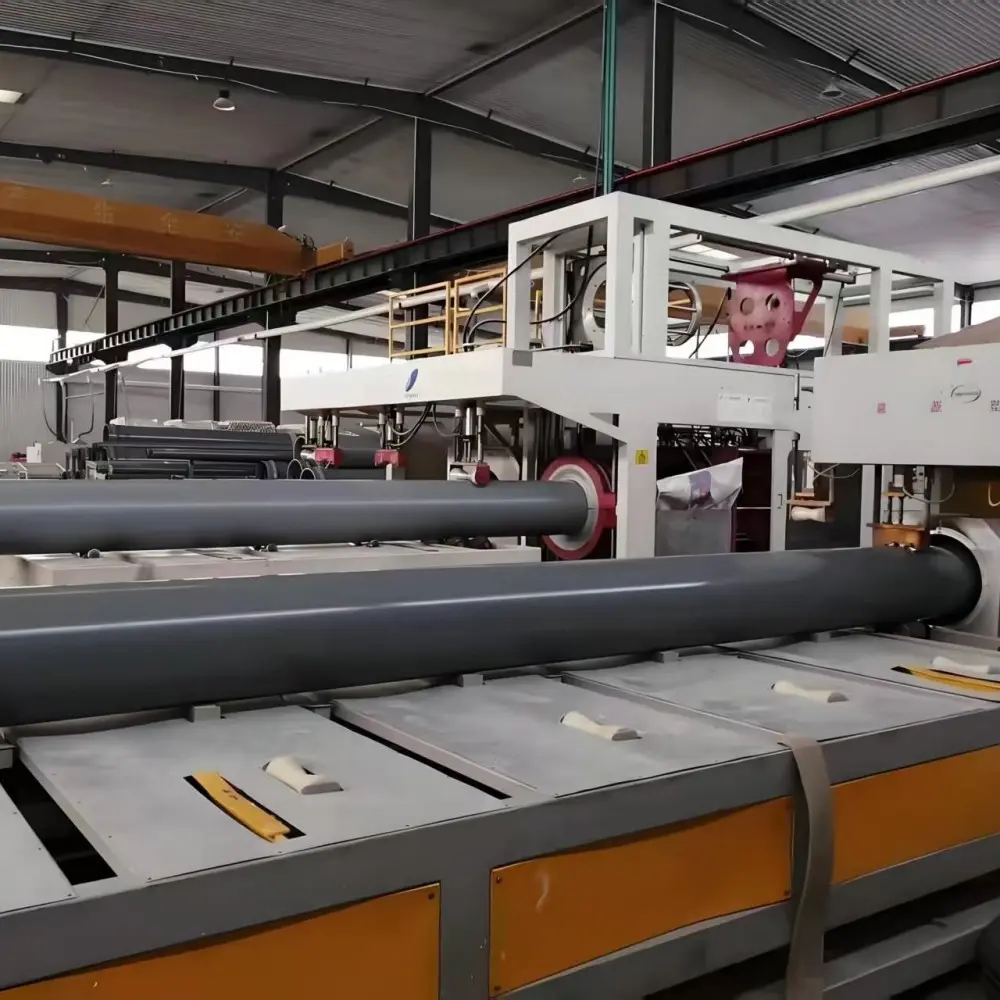
Plastic Piping & Conduit Lines
PVC-U, CPVC, and HDPE pipeline systems designed for potable municipal water supply, agricultural drainage, and telecommunication conduits.
Request an Official CE Certified Wire Rod Quotation
Our international engineering trade directors review specifications, mechanical requirements, and Incoterm logistics within 24 business hours.
Headquarters & Industrial Cluster
Tianjin Huizhong Xinyu International Trade Co., Ltd. (HZXY)
Sanding Logistics Park, 500 m north of Tuanda Rd & Jinwang Rd intersection, Daqiuzhuang, Jinghai District, Tianjin, China.
Dual production bases located in Tianjin and Tangshan with dedicated rail siding and fast dispatch access to Tianjin Port.
Direct Commercial Lines
- Direct Phone: +86 176 9548 5299
- Executive Email: [email protected]
- Direct WhatsApp: +86 189 2063 7962
English, Spanish, and Russian speaking commercial coordinators assigned to each international project tender.
Catalog & Specification Resources
Download our complete 2026 steel profiles, coil parameters, wire rod metallurgy handbooks, and standard tolerance guidelines.