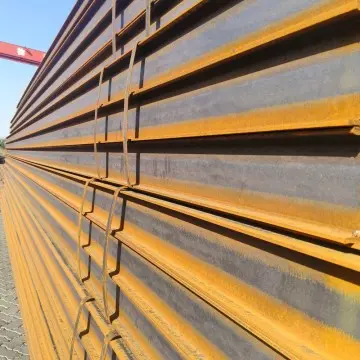
A36 / Q235 Grade Structural H-Beam
Hot-rolled structural columns and beams serving as primary substrates for CE-marked heavy-duty self-drilling fastener anchoring.
View H-Beam QuotesSelf-tapping screws achieve specified load capacities only when matched with certified structural steel substrates. Explore our core in-stock steel profiles and coils engineered to EN 10025, ASTM, and GB standards.
Hot-rolled structural columns and beams serving as primary substrates for CE-marked heavy-duty self-drilling fastener anchoring.
View H-Beam Quotes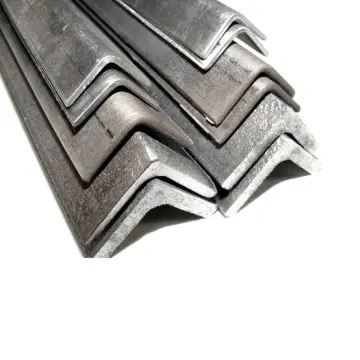
Precision-punched equal and unequal angle sections optimized for mechanical bracing, secondary steel, and rapid screw assembly.
Explore Angle Steel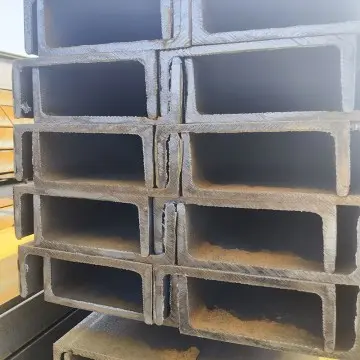
U and C channel structural sections manufactured for facade purlins and side framing, providing consistent pull-out pull-over resistance.
Check Channel Steel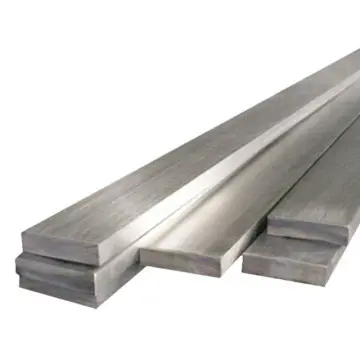
Solid mill-finish and galvanized flat steel engineered for structural connection brackets, base plates, and earthing clips.
Inspect Flat Steel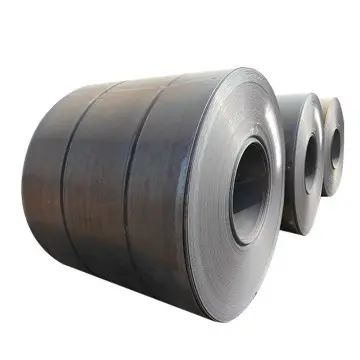
Structural master coils slit to tight width tolerances for roll-forming cold-formed steel (CFS) studs and light metal purlins.
Access Coil Pricelist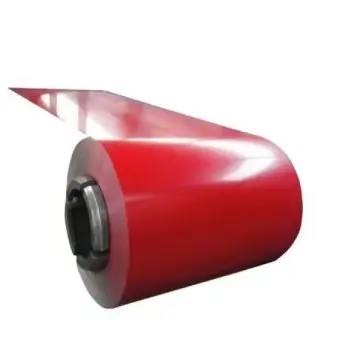
RAL-specified color-coated coil for sandwich panels and roofing sheets, requiring EPDM washer self-drilling screws for weatherproofing.
Explore PPGI Range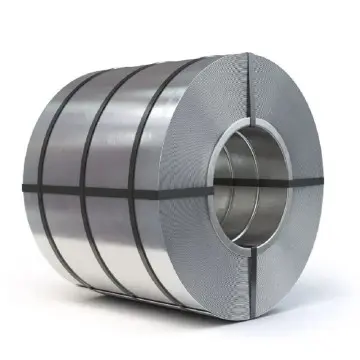
Continuous hot-dip galvanized strip with Z100–Z275 coating weights, ideal for roll-formed drywall tracks and structural purlins.
Review DX51D Specs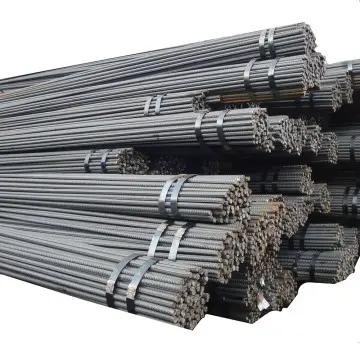
High-yield ribbed carbon steel reinforcement rods for concrete structures, foundations, slabs, and prefabricated modular cages.
Get Rebar DetailsProcuring self-tapping and self-drilling screws for the European Economic Area (EEA) requires strict adherence to harmonized European Norms. CE marking is not merely a quality stamp; it is a legally binding declaration of conformity.
Under System 3 Assessment and Verification of Constancy of Performance (AVCP), the fastener manufacturer must maintain an internal Factory Production Control (FPC) system that continuously audits raw wire chemistry, dimensional tolerances (DIN 7504, ISO 15480), thread geometry, and heat treatment stability. Initial Type Testing (ITT) conducted by a notified laboratory serves as the empirical foundation for the manufacturer's Declaration of Performance (DoP). Sourcing from non-certified trading entities without traceable FPC records voids site insurances and violates Eurocode 3 (EN 1993-1-3) structural assembly standards.
| Harmonized Standard / Guideline | Applicable Scope | AVCP System | Mandatory Mechanical Testing Attributes | CE Documentation Required |
|---|---|---|---|---|
| EN 14566:2008+A1:2009 | Gypsum board drywall metal framing, ceiling suspensions | System 4 / System 3 | Drill speed verification (≤ 2.5s), flexural bending (≥ 15°), pull-out capacity | CE Labeling, DoP, Dimensional Certificate |
| EN 14592:2008+A1:2012 | Timber construction, structural wood-to-metal connections | System 3 | Yield moment ($M_{y,k}$), withdrawal parameter ($f_{ax,k}$), tensile capacity ($f_{tens,k}$) | Notified Body ITT Report, DoP, 3.1 MTR |
| EAD 330046-01-0602 (ETA) | Fastening screws for metal members and sheeting (purlins, roofs) | System 2+ | Shear load ($V_{R,k}$), tension load ($N_{R,k}$), design resistance to cyclic thermal shock | ETA Certificate, Notified FPC Audit, DoP |
| ISO 10666 / DIN 7504 | Drilling screws with tapping screw threads | Industrial Norm | Torsional strength ratio ($T_{break} \ge 1.5 \cdot T_{drive}$), core hardness (320–400 HV) | EN 10204 Type 3.1 Inspection Certificate |
Structural self-tapping screws endure severe torsional friction, extreme shear stresses, and harsh atmospheric microclimates. Engineering failure is avoided at the atomic level through disciplined metallurgy.
Standard carbon steel screws rely on cold-heading quality (CHQ) wire rod. Continuous carburizing mesh-belt furnaces impart a surface hardness of 560–650 HV to penetrate heavy steel purlins, while maintaining a ductile core (320–400 HV) to absorb dynamic structural vibrations without brittle fracture.
To eliminate bimetallic galvanic corrosion in outdoor architectural envelopes, bi-metal screws fuse an AISI 304 (A2) or AISI 316 (A4) stainless steel shank with an induction-welded case-hardened alloy carbon drill tip. This delivers self-drilling velocity through steel up to 12.5mm thick with lifelong atmospheric rust immunity.
Electroplating high-strength fasteners can trap atomic hydrogen within the crystalline lattice, causing catastrophic delayed failure under tension. HZXY executes automated post-plating thermal baking at 200°C ± 5°C for 4 to 8 hours within 1 hour of acid pickling to desorb trapped hydrogen atoms.
Where standard electro-galvanizing (5–8 μm) fails salt spray tests at 72–120 hours, multi-layer organic zinc flake and Ruspert ceramic systems provide 1,000 to 2,500 hours of neutral salt spray testing (ISO 9227) without red rust, eliminating acid pickling to completely prevent hydrogen embrittlement risks.
Fastener performance depends on regional wind loads, seismic classifications, atmospheric humidity, and dissimilar metal pairings. We engineer fastening assemblies tailored to four major industrial scenarios.
Utility-scale PV solar installations in desert, coastal, and agricultural terrains demand fasteners that withstand continuous wind buffet and thermal expansion. Fastening module clamps to roll-formed galvanized C/U purlins requires heavy-gauge bi-metal fasteners equipped with conductive tooth-lock washers to maintain continuous electrical grounding and withstand micro-fretting wear over a 25-year design life.
Off-site prefabrication and modern methods of construction (MMC) utilize 0.75mm–1.5mm high-tensile cold-formed steel studs (G550 / S350GD). Fasteners require low-profile wafer or modified truss heads with undercut knurling to avoid bulging gypsum drywall boards, while micro-drill points (Point #1 and #2) prevent stud stripping during high-RPM automatic robotic screwdriving.
Composite PIR/PUR/Mineral Wool roof and wall cladding panels (40mm to 200mm thickness) require specialized dual-thread self-tapping screws. The primary thread anchors solidly into the structural steel sub-purlin, while an enlarged secondary thread under the head securely clamps the outer profiled metal skin, preventing panel dimpling, water pooling, and seal fatigue over seasonal thermal cycles.
Architectural unitized facades link extruded aluminum brackets (6063-T6) to structural carbon steel anchor plates embedded into reinforced concrete. Screws must combat thermal-induced shear displacements and catastrophic galvanic reaction. AISI 316 bi-metal self-drilling screws treated with specialized non-conductive barrier coatings protect against electrolyte-driven galvanic degradation.
Positioned within the world’s most dense steel production cluster in Tianjin and Tangshan, HZXY delivers unmatched cost-efficiency, continuous wire supply, integrated heat treatment, and rapid container dispatch.
Located in Daqiuzhuang, Jinghai District, Tianjin, our direct physical proximity to primary blast furnaces and wire-rod continuous casting mills ensures constant access to prime SAE 1006, 1008, 1022A, and 10B21 raw steel coils. Eliminating intermediate domestic transit shields international buyers from speculative spot-market volatility.
Modern cold forging lines combine multi-die cold heading with high-precision thread rolling machines operating at speeds up to 350 pieces per minute. Automated optical sorting machines inspect head concentricity, recess depth, thread pitch, and drill point sharp radius, ensuring < 50 PPM defect rates for robotic assemblies.
Rather than sub-contracting heat treatment, continuous atmospheric-controlled mesh belt furnaces precisely modulate carbon potential ($C_p$), soaking temperatures, and quenching oil viscosity. This guarantees uniform carburization depth and avoids surface decarburization, ensuring high torsional break resistance.
Buyers can consolidate structural H-beams, hollow sections, PPGI coils, drainage pipes, and multi-pallet CE-certified fasteners in a single bill of lading from Tianjin Port. This consolidated shipping model slashes port handling surcharges, brokerage fees, and supply line coordination overhead.
International procurement managers face shifting geopolitical tariffs, Anti-Dumping Duties (ADD), and carbon border adjustment taxes (CBAM). Sourcing safely requires documented supply chain transparency.
The European Commission and US Department of Commerce maintain specific tariff classifications on iron or steel fasteners (CN code 7318 14). Partnering with compliant Chinese manufacturers who provide verifiable Factory Production Control (FPC) and transparent cost-of-production audits ensures seamless customs entry and prevents unexpected retroactive tariff liabilities.
With the phase-in of the European Carbon Border Adjustment Mechanism (CBAM), embedded emissions for carbon steel wire rod products must be documented. HZXY works closely with regional EAF (Electric Arc Furnace) and modern converter steelmakers in Hebei to monitor specific embodied carbon ($tCO_2e/t$), providing preliminary reporting data to European importers.
Every carton and pallet features serialized 2D Matrix barcodes detailing the mother coil heat number, cold-heading machine run, heat treatment furnace batch, and surface coating chamber lot. EN 10204 Type 3.1 Inspection Certificates accompany all exports, detailing certified chemical composition, tensile strengths, core hardness, and torque test curves.
Before issuing an EN 14566 or EN 14592 CE Declaration of Performance, every production lot undergoes six essential laboratory tests to guarantee zero on-site failure.
| Testing Protocol | Reference Standard | Test Parameters & Rig Setup | CE Minimum Compliance Threshold |
|---|---|---|---|
| Drilling Speed & Penetration | EN 14566 / ISO 10666 | Motorized drill test stand at constant 2500 RPM with axial load of 150 N – 250 N through cold rolled test sheet | Complete tap & penetration achieved in ≤ 2.5 seconds without thread galling |
| Torsional Strength ($M_t$) | ISO 10666 / DIN 7504 | Screw clamped in split threaded collet with unthreaded tip exposed; calibrated torque wrench rotated until fracture | $M_{break} \ge 1.5 \times M_{drive}$ (Minimum breaking torque table per shank diameter) |
| Tensile Pull-Off ($F_{tens}$) | EN ISO 898-1 / EN 14592 | Hydraulic universal tensile frame gripping screw head underside and shank thread engagement until ultimate yield | Must exceed characteristic tensile capacity specified in DoP (e.g., ≥ 4.5 kN for 4.8mm shank) |
| Surface & Core Hardness | ISO 6507-1 / ASTM E384 | Micro-Vickers hardness tester with 0.3 kgf load ($HV_{0.3}$) on polished metallurgical cross-section mounts | Surface Hardness: 560–650 HV; Core Hardness: 320–400 HV; Transition zone > 0.05 mm |
| Neutral Salt Spray (NSS) | ISO 9227 / ASTM B117 | Continuous 5% NaCl atomized mist cabinet at 35°C ± 2°C, inspected every 24 hours for corrosion formation | Zinc 5μm: 72h white/120h red; Ruspert 1000h: zero red rust; Stainless: 2000h+ clear |
| Hydrogen Embrittlement Test | DIN 50969-2 / ASTM F1940 | Fasteners torqued to 80% of mean torsional fracture against hardened steel plate and held under static strain for 48 hours | Zero heads fractured or cracked after 48 hours continuous pre-stress load |
The structural fastener industry is shifting toward smart automated installations, environmentally safe passivation, and high-strength alloy compositions.
Complying with strict EU REACH directives, hexavalent chromium coatings have been fully phased out. R&D now targets thin-film organic coatings infused with nano-graphene platelets, providing self-healing barrier protection that resists thread damage during high-speed insertion.
As modular construction shifts toward automated robotic gantry systems, fasteners require ultra-precise collation tapes, tightened head tolerances, and optimized drill geometry. This enables jam-free robotic driving at speeds up to 4,000 RPM into high-tensile steel framing.
Next-generation cold heading utilizes micro-alloyed boron steels with titanium and vanadium micro-additions. This delivers 1,200 MPa tensile strength while maintaining cold-impact ductility down to -40°C, ideal for arctic infrastructure and offshore wind installations.
Tianjin Huizhong Xinyu (HZXY) bridges Chinese manufacturing efficiency with stringent project standards worldwide through direct engineering support and documented quality assurance.
Every order is assigned a bilingual fastener engineer with 5+ years of international EPC experience. Our team assists with joint calculation reviews, screw pull-out estimations per Eurocode 3, and equivalent grade cross-matching between GB, EN, ASTM, and JIS standards.
Contact Engineering TeamBuyers can commission independent inspection agencies (SGS, Bureau Veritas, TÜV Süd, Intertek) prior to container loading at our Tianjin facility. Inspections include chemical spectrographic analysis, thread dimensional checks, plating thickness tests, and mechanical tensile breaks.
Request Quality DossierFasteners can be packaged in custom-branded private label cartons, heavy-duty weather-sealed plastic buckets, or bulk industrial bins. Every unit features scannable EAN/UPC barcodes, CE conformity marks, batch IDs, and multi-language technical warning labels for direct job-site distribution.
Browse Packaging OptionsCombine structural pipes, cold-heading quality wire rods, solid bars, and project valves in a single consolidated shipment from HZXY's Tianjin and Tangshan production bases.
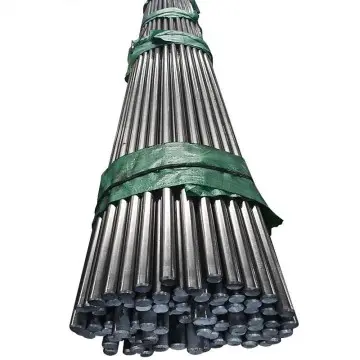
Smooth carbon solid steel bars designed for structural tie-rods, dowels, architectural bracing, and heavy hardware fabrication.
View Round Bar
High-carbon and low-carbon coiled wire rod serving as raw material feed for drawing wire, re-rolling, springs, and industrial fasteners.
Review Wire Rod
Accurate-diameter, low-carbon bright wire optimized for nail production, cold-forged fasteners, mesh, and wire forming.
Explore Cold Drawn Wire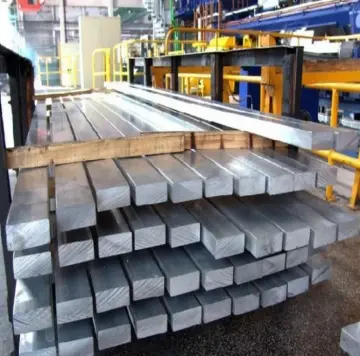
Heavy-duty zinc-coated flat sections (3–60 mm thickness) for outdoor earthing grids, structural connections, and brackets.
Check HDG Flat Bar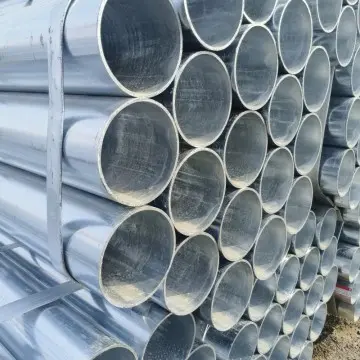
Welded circular structural steel tubing with high-adhesion zinc finish for construction scaffolding, greenhouse frames, and railings.
Inspect Scaffolding Pipe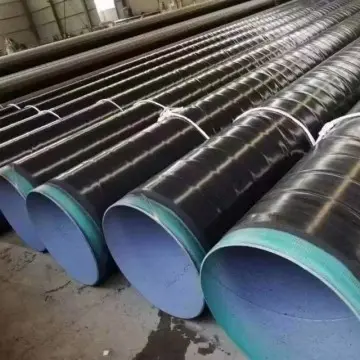
Heavy-wall industrial pipeline steel with multi-layer exterior protective coatings for pressurized civil and industrial fluid transmission.
Explore Coated Pipe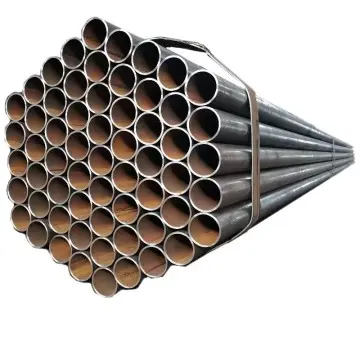
Standard ERW plain-end and beveled black steel pipes for structural columns, low-pressure fluids, and site fabrication.
View Black Pipe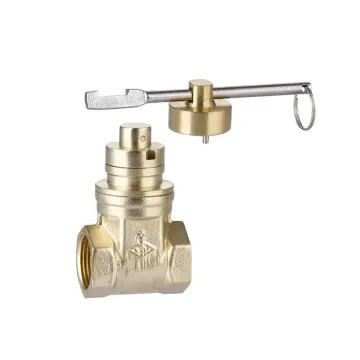
Gate, globe, ball, check, and butterfly valves precision-matched to our steel piping lines for HVAC, water supply, and gas systems.
Browse Valve RangeDirect technical answers for commercial procurement officers, quality control auditors, and structural engineers specifying industrial self-tapping screws.